 EN — English
 TR — Türkçe
 DE — Deutsch
 RU — Русский
 FR — Français
 ES — Español
 AR — العربية
 SR — Српски

Maintenance and Wear
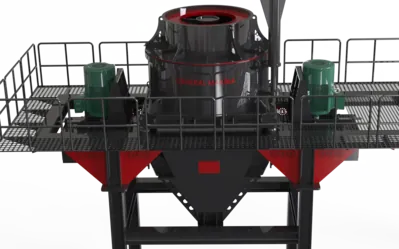
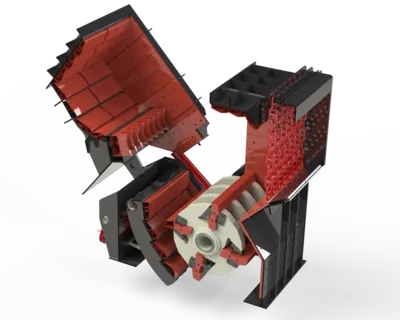
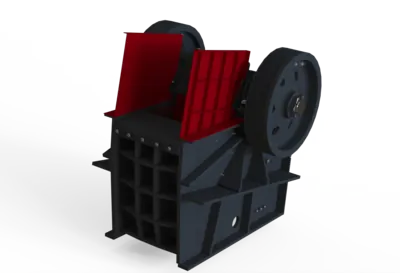
Maintenance and wear: where a crushing plant actually spends its money
The purchase price of a crusher is a small share of what the machine will cost across its working life. Three items decide the real cost per tonne: energy, wear parts and downtime. Two of those three sit on the maintenance engineer's desk. Change a wear part too early and money is thrown away; change it too late and the frame, the rotor or the housing is put at risk. The way out is not better guessing but measurement. This section explains which numbers maintenance decisions rest on, from lubrication and bearing temperature to alloy selection and spare part stocking policy.
The underlying logic is straightforward. Every wear part has a measurable consumption rate, every bearing has a stable temperature signature, and every drive group has an acceptable vibration band. The day those three signatures are recorded is the day unplanned downtime starts turning into planned downtime.
Lubrication planning and grease selection
Most bearing failures in crushers and screens are not caused by an absence of grease but by the wrong grease practice. It appears in three forms: too much, too little, and incompatible. Excess grease fills the free space in the bearing so that the grease mass itself becomes a friction source and the housing runs hotter. Insufficient grease breaks the oil film and allows metal-to-metal contact. Incompatible greases soften when two different thickeners are mixed, and the mixture simply leaks out of the housing.
What the consistency grade tells you
Grease consistency is classified by worked penetration. The value is measured at 25 °C after 60 double strokes in a grease worker and reported in tenths of a millimetre. A higher penetration figure means a softer grease.
| NLGI grade | Worked penetration (0.1 mm) | Consistency | Typical plant use |
|---|---|---|---|
| 000 | 445-475 | Fluid | Centralised lubrication lines, gearboxes |
| 00 | 400-430 | Semi-fluid | Centralised systems with long runs |
| 0 | 355-385 | Very soft | Automatic lubricators in cold climates |
| 1 | 310-340 | Soft | Automatic systems with long feed lines |
| 2 | 265-295 | Normal | The majority of rolling bearing housings |
| 3 | 220-250 | Firm | High temperature, vertical shafts, leak-prone housings |
| 4 | 175-205 | Very firm | Applications needing special sealing |
| 5 | 130-160 | Hard | Rare, open gear applications |
| 6 | 85-115 | Block | Effectively unused in modern plants |
In crushing and screening the practical decision space narrows to grades 1, 2 and 3. A softer grade suits a central pump pushing grease through long lines; a firmer grade suits vertical shaft machines and hot housings. Grade alone is not a specification: base oil viscosity, thickener type and extreme pressure additives must match the duty as well. Term definitions are collected in the technical glossary.
Correcting the relubrication interval for temperature
Grease ages faster as housing temperature rises, and the established engineering rule is specific. Above 70 °C, the relubrication interval is halved for every 15 °C of additional temperature, up to the high temperature limit of the grease. Below 70 °C the interval may be doubled for a 15 °C reduction, but that extension is applied only once. Full complement bearing types and thrust arrangements are not given an extended interval at all. Vertical shafts and continuous vibration shorten the interval. This correction is the single step that ties a catalogue interval to the real temperature on site, and skipping it leaves the lubrication plan on paper only.
Tracking bearing temperature
A bearing temperature reading means little on its own; the information lives in the trend. A vibrating screen bearing that holds a 58-62 °C band for weeks under the same feed and ambient conditions has a healthy signature. The same bearing climbing from 62 °C to 78 °C across two shifts demands attention even while the absolute figure still looks tolerable. For that reason readings belong to a continuous series tied to a bearing number, not to a shift logbook.
| Observation | Interpretation | Maintenance action |
|---|---|---|
| 20-40 °C above ambient, stable | Normal running signature | Record only |
| Housing above 70 °C | Grease ageing accelerating | Halve the interval per 15 °C of rise |
| More than 10 °C jump within 48 hours | Over-greasing, load shift or early damage | Check grease quantity and vibration spectrum |
| 15 °C difference between two bearings on one shaft | Alignment or clearance error | Measure coupling alignment and housing seating |
| Temperature rose further after greasing | Excess grease or consistency mismatch | Purge the housing and refill with the correct grade |
The measuring point must be identical every time. The natural spread between different areas of one housing is wide enough to hide a real trend. In stationary installations the measurement route is defined once and stays fixed for the life of the machine; in a quarry stationary plant layout the most effective solution is to mark the points permanently on the structure.
Measuring wear part life
Saying that a jaw plate lasts three months is not a measurement. The calendar is a consequence of wear, not its cause. The real unit of wear is processed material, so a single figure is kept for each wear part: part mass consumed per tonne. The method is simple. Weigh the part when it goes in, weigh it again when it comes out, and read the tonnage that crossed the weighbridge in between. Divide lost mass by tonnage.
Three doors open once that number exists. First, castings from different foundries can be compared on performance rather than on price. Second, the effect of a feed change becomes visible: a wetter, more clay-bearing feed on the same jaw crusher shifts the consumption rate noticeably. Third, replacement moves off the calendar and onto a threshold. Remaining section is measured, and when the critical thickness is reached the part is changed during a planned stop.
Three methods work together: mass tracking, profile checks against a template, and thickness readings in critical zones. The distribution of the loss carries information too. Wear concentrated in one zone comes from feed distribution rather than casting quality, and replacing the part does not fix it.
Manganese steel and alloy selection
The classic material for crushing surfaces is austenitic manganese steel, and its defining property is that the surface hardens under impact. After solution heat treatment and water quenching, the casting is delivered at roughly 200-225 HB, meaning it arrives soft. Given sufficient impact in service the surface layer rises above 500 HB while the core keeps its tough austenitic structure. The hardening mechanism is deformation twinning. One critical consequence follows: manganese steel does not harden without impact. Fitting manganese into a low-impact, purely abrasive duty produces a part that wears away without ever reaching its working hardness.
The composition envelope for austenitic manganese castings is standardised. The common base grade is defined as carbon 1.05-1.35 %, manganese 11.0 % minimum, silicon 1.00 % maximum and phosphorus 0.070 % maximum; in practice manganese usually sits in the 11-14 % band. Variants with chromium, molybdenum or nickel additions are used where higher yield strength or better behaviour in thick sections is needed.
When impact is low and abrasion is high, the choice moves to high chromium white iron. The common grade containing 14.0-18.0 % chromium and up to 3.0 % molybdenum can be heat treated to 56 HRC and above, while as-cast hardness typically falls in the 450-550 HB band. Molybdenum is there not for hardness itself but so that thick sections harden through. The high carbide volume makes this material extremely abrasion resistant and correspondingly brittle under impact.
| Material family | Composition envelope | Hardness | Suitable wear regime |
|---|---|---|---|
| Austenitic manganese steel, base grade | C 1.05-1.35 %, Mn 11.0 % min, Si 1.00 % max, P 0.070 % max | 200-225 HB as delivered, surface above 500 HB | High impact: jaw plates, concaves, mantles |
| Manganese with chromium or molybdenum | Base grade plus alloying additions | Similar as delivered, higher yield strength | Thick sections under high impact |
| High chromium white iron | Cr 14.0-18.0 %, Mo up to 3.0 % | 450-550 HB as cast, 56 HRC minimum when hardened | Low impact, high abrasion: tertiary duty, shell liners |
At the secondary stage material choice cannot be separated from machine choice, because the crushing principle sets the impact regime. That relationship is worked through step by step in the cone versus impact secondary crusher selection comparison, and the matching machine can be picked from the crusher range. The same reasoning governs cone crusher cavity parts and primary impact crusher blow bars.
Vibration analysis and the acceptance band
Vibration measurement is the most direct way to see the condition of rotating groups before damage forms. Readings are taken on non-rotating parts, typically the bearing housing, and evaluated as overall RMS velocity across the 10-1000 Hz range. For medium sized electrical machines, meaning 15 kW to 300 kW of power or shaft heights of 160-315 mm, mounted on a rigid foundation, the acceptance band divides as follows:
| Zone | RMS velocity (mm/s) | Meaning | Operating decision |
|---|---|---|---|
| A | 1.4 and below | Level of a newly commissioned machine | Record as the reference value |
| B | 1.4-2.8 | Acceptable for unrestricted long-term running | Routine monitoring |
| C | 2.8-4.5 | Unsatisfactory, running time should be limited | Find the cause, schedule a planned stop |
| D | Above 4.5 | Unacceptable, capable of causing damage | Intervention takes priority |
Machines on flexible mountings are allowed higher values because the mounting adds damping, and confusing the two columns is a common field error. The band is guidance; a machine's own history and the direction of its trend are stronger signals than an absolute threshold. A unit that has run at 2.1 mm/s for months and now reads 3.0 mm/s has changed, even though it remains far from zone D.
Building a planned downtime calendar
Planned downtime is not lost production, it is protected production. The logic behind the calendar is never to open the same housing twice. Everything that will be done during one stop goes on one list: wear part replacement, grease renewal, belt splice and tension checks, drive alignment, sealing elements. Jobs with a known duration and parts already on the shelf go on that list; jobs whose diagnosis is unfinished do not, because what stretches a stop is uncertainty rather than the number of tasks.
The calendar draws on three inputs: the remaining life produced by wear measurement, the early warnings implied by temperature and vibration trends, and the window the production programme allows. When those three come together, the stop happens at a time the operation chooses instead of a time a broken part dictates. Splice inspection on conveyor belt lines and structural bolt torque checks on a stationary crushing plant are two jobs best combined in the annual major stop.
To see the cost side of downtime, the maintenance share per tonne has to enter the arithmetic; the operating cost calculator places that share alongside energy and wear items.
Setting spare part stock levels
A stocking policy has to answer two questions together: does the plant stop without this part, and how long does the part take to arrive. The intersection of the two answers is the decision. Parts that stop production and have long lead times are held on the shelf. Holding stock of a part that neither stops production nor takes long to obtain simply ties up capital.
For wear parts the stock level follows from the consumption measurement. Once monthly tonnage and measured consumption rate are known, the quantity that covers the lead time falls out of the arithmetic. Critical but inexpensive items such as bearings, seals and couplings follow a different rule: they are stocked according to the cost of their absence rather than their own price. Compatible dimensions and housings are confirmed against the crusher spare parts list and the wider spare parts group.
Everything in this section serves one habit: never replace without measuring, and never wait once you have measured. If you want your own wear and lubrication plan reviewed against your existing records, send your operating data to our engineering team and we will work out remaining life and stock levels with you.
Frequently Asked Questions
How hot may a crusher bearing housing run?
There is no single ceiling worth quoting; the trend matters more. A housing holding steady at 20-40 °C above ambient is normal. Once it passes 70 °C the grease ages faster, so the relubrication interval is halved for every further 15 °C.
What unit should I use to track wear part life?
Not the calendar, but part mass consumed per tonne processed. Weigh the casting on installation and on removal, read the tonnage that passed the weighbridge in between, and divide the lost mass by that tonnage. It is the only honest basis for comparing suppliers on performance instead of price.
Is manganese steel the right choice at every crushing stage?
No. Austenitic manganese steel only hardens where it receives real impact; it arrives at roughly 200-225 HB and climbs above 500 HB in service. In low impact, high abrasion duty that hardening never happens, and high chromium white iron delivers longer life instead.
Which NLGI grade should I specify?
Crushing and screening duty narrows the practical choice to grades 1, 2 and 3. Long centralised lines favour a softer grade, while vertical shaft machines and hot housings favour a firmer one. Consistency is only part of the specification: base oil viscosity and thickener type must also suit the duty.
At what vibration level should we act?
For medium machines of 15-300 kW on rigid foundations, below 1.4 mm/s is new-machine condition and 1.4-2.8 mm/s is acceptable for unrestricted running. Between 2.8 and 4.5 mm/s running time should be limited while the cause is found; above 4.5 mm/s is unacceptable.
How do I decide what to keep in stock?
Cross two answers: whether the plant stops without the part, and how long it takes to arrive. Items that halt production and have long lead times stay on the shelf. For wear parts the quantity comes from measured consumption per tonne multiplied by monthly tonnage over the lead time.