EN — English
 TR — Türkçe
 DE — Deutsch
 RU — Русский
 FR — Français
 ES — Español
 AR — العربية
 SR — Српски

Cone crusher hydraulic and lube system maintenance
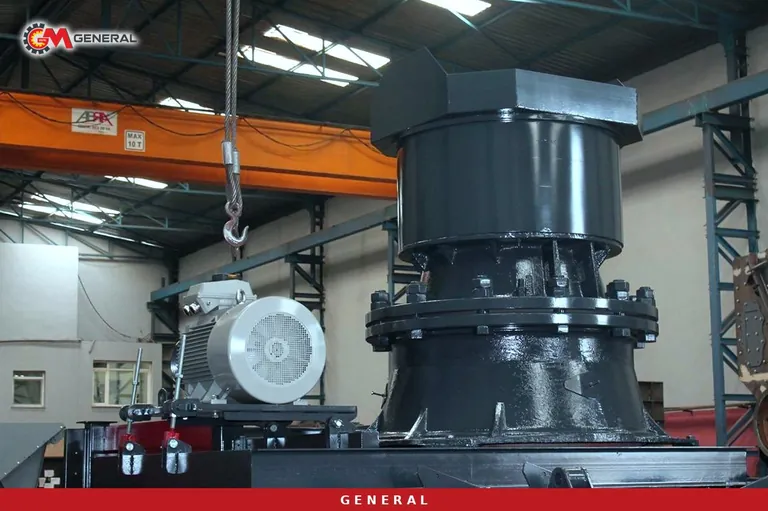
One machine, two independent circuits
Cone crusher hydraulic and lube system maintenance goes wrong from the outset when it is treated as the upkeep of a single fluid circuit. The machine carries two separate circuits whose duties and requirements do not overlap. The lubrication circuit feeds bronze bushings, the shaft bearing and the gear set; it needs continuous flow, heat removal and cleanliness. The hydraulic circuit drives setting adjustment and overload protection; it needs fast response, stable pressure and tight sealing. That is why the two circuits take fluids from different viscosity grades and are never substituted for one another.
The temperature window on the lube circuit
The health of the lubrication circuit is read fastest from return oil temperature. In practice the window generally accepted runs roughly from 38 to 55 degrees Celsius; some systems tolerate a wider band, but that range is treated as the target for machine health. What matters more than the absolute number is behaviour. A return temperature that climbs steadily while feed and ambient conditions stay unchanged points to restricted flow, growing internal wear or a cooler that is no longer doing its job. For the same reason the difference between supply and return is tracked as well: if the difference narrows, the oil is no longer carrying heat away.
Cold starts
In cold weather neither the oil pump nor the main motor is started before the oil reaches the temperature the manufacturer specifies. Cold, thick oil does not reach the bushings in time, and that produces damage far faster than running hot ever does. A reservoir heater and a temperature interlock matter as much through winter as any high-temperature alarm.
| Parameter | Practical target | What a deviation indicates |
|---|---|---|
| Return oil temperature | Roughly the 38-55 °C band | Rising: restricted flow, internal wear, cooler fault |
| Supply to return difference | Steady and repeatable | Narrowing: falling flow, internal leakage |
| Oil temperature before start | Above the manual's lower limit | Starting below it: bushing starvation |
| Filter differential pressure | Low and stable on a clean element | Rising: element loading, bypass risk |
| Reservoir level | Within the marked range | Falling: leakage; rising: hydraulic oil crossing over |
Cleanliness: filters, codes and sampling
The quietest variable governing component life on a cone crusher is contamination. Oil cleanliness is expressed as a three-number code built from particle counts above different size thresholds, reported for the 4, 6 and 14 micrometre thresholds. The code is not a target in isolation; it is read as a trend. On the same machine under the same duty, a code that deteriorates says either that the filter element has loaded up or that dust is finding a way in.
Where the sample is drawn
Samples are drawn from an active return line on a running system. A sample taken from the bottom of the reservoir shows settled material, does not represent the state of the system, and makes comparison between reports impossible into the bargain. The sampling point is chosen once and used every time.
Reading the analysis
Elemental analysis usually names the wearing part without any need to strip the machine. Rising copper and tin point to bronze bushing wear, rising iron to the gear set or a shaft surface, and rising silicon to dust ingress, which means a seal or a filtration problem. No single report decides anything; a trend across two or three samples does.
| Rising value | Likely source | First action |
|---|---|---|
| Copper, tin | Bronze bushing wear | Measure clearances, review load and temperature history |
| Iron | Gear set or shaft surface | Inspect tooth contact pattern, take vibration readings |
| Silicon | Dust ingress | Check seals, breather filter and reservoir covers |
| Water content | Cooler or condensation | Check cooler tightness and reservoir breathing |
The hydraulic circuit and overload protection
The hydraulic circuit does two jobs: it changes the setting, and it lets an uncrushable object pass. The second function begins when tramp material enters the chamber and pressure spikes; the accumulator compresses, the moving cone lifts and the object passes through. Whether that chain works at all depends on the nitrogen pre-charge in the accumulator. If pre-charge falls away or the bladder ruptures, the system can no longer soften the event and the load transfers into the structure instead of being relieved. Pre-charge is therefore measured on a schedule and recorded, with the measurement taken after the accumulator has been discharged on the hydraulic side.
A machine does not return to its previous setting by itself once an object has passed; the setting is re-established and the chamber inspected. Repeated overload events in quick succession say the fault lies in the feed rather than the hydraulics: scalping, magnetic separation or feed size deserves review. Chamber selection belongs in that picture too, because a cone crusher fed coarser than its chamber accepts will trip protection continuously.
Stopping, starting and the record that ties it together
A machine is not stopped under load; the chamber is cleared first, otherwise the motor and drive are punished on the next start. After shutdown the oil pump keeps running for a period so heat can be drawn out of hot surfaces. For any of this to mean something, one record set is needed: return temperature and filter differential every shift, oil analysis result and accumulator pre-charge every period, and an entry for every overload event. Placed side by side, those three lines show a failure before it arrives. Related maintenance topics are collected under maintenance and wear.
Frequent questions
Can the same oil serve both circuits?
No. The lubrication circuit needs a more viscous product that will hold a film under shock loading, while the hydraulic circuit needs a thinner one so valves and accumulator can respond quickly. The two requirements are listed separately in the machine manual.
Return temperature is just under the limit. Keep running?
Trend matters as much as the number. If the temperature is climbing steadily, the cause is investigated before the limit is reached: cooler matrix, oil flow and filter condition are the first places to look.
When is accumulator pre-charge checked?
On the planned interval and after every significant overload event. A protection system going quietly out of service is only discovered when that measurement is actually taken.
Definitions of technical terms: Glossary