EN — English
 TR — Türkçe
 DE — Deutsch
 RU — Русский
 FR — Français
 ES — Español
 AR — العربية
 SR — Српски

Supplier factory audit and pre-shipment inspection
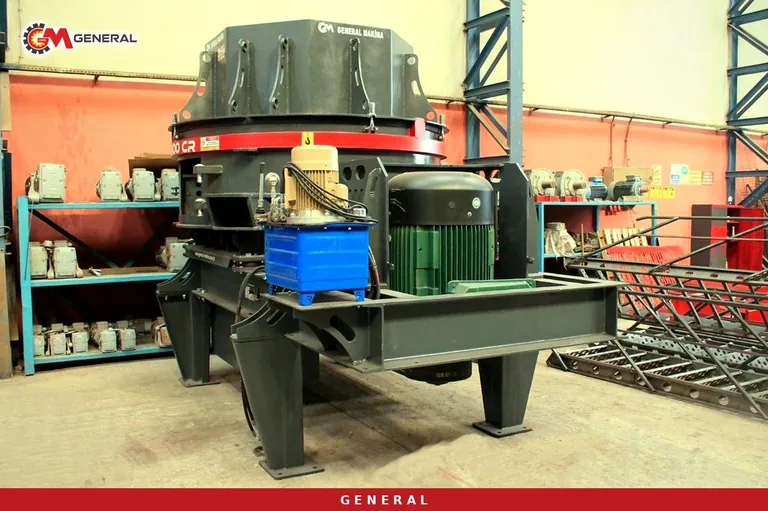
On a machine bought at distance, the expensive surprise arrives when the crates are opened on site rather than at the port. A supplier factory audit and pre-shipment inspection moves that surprise back into the middle of production, while correction is still possible. The two exercises are routinely confused although they answer different questions: one looks at how the manufacturer works, the other at what is actually going into the crate.
An audit tests the system, an inspection tests the product
A factory audit is a second-party audit: the buyer examines the supplier's processes against its own contract. Its scope covers the production flow, calibration of measuring equipment, material traceability, use of subcontractors, how non-conforming product is segregated and whether corrective actions are recorded. Inspection, by contrast, measures defined characteristics of one specific product. A clean audit does not remove the need for inspection, and a clean inspection does not make the audit unnecessary on the next order.
What is worth looking at during the visit
Finished machines on display tell you very little. The revealing areas are the intermediate ones. In plate cutting and frame welding you see the welding sequence and the measures taken against distortion. In blasting and painting you learn how surface preparation is done and under what conditions the coating cures. On the assembly line there is really one question: where does each component come from and is that recorded? Without traceability, nobody can answer which steel a failed shaft was made from a year later.
How the production flow is organised at General Makina is described on the how we work page, and reading that kind of description before a visit sharpens the questions worth asking.
Two measurable items: welds and paint
Welds are examined visually, with sufficient illumination and physical access, while the limits for acceptable imperfections depend on the quality level named in the contract. That scale has three levels, and which one applies is decided by the purchaser, not by the standard. When the specification is silent on the level, an argument during inspection is guaranteed.
For paint the measured quantity is dry film thickness. On rough surfaces such as blasted steel, peaks and valleys skew individual readings, so sampling and evaluation rules are defined separately. What the buyer should ask for is not a single reading but the list of measurement points and the calibration record of the gauge.
The habit of reading nameplates
Whether the components named in the offer are really those brands can only be established from the nameplate. Serial numbers of main motors, gearboxes and large bearings are photographed and compared with the order documents. This is not distrust but an ordinary acceptance step, and it shortens the warranty process when something fails on site.
The no-load run
The most valuable test available before shipment is running the machine unloaded at the works. What has to be recorded is well defined: direction of rotation, abnormal noise, the trend of bearing temperatures, current draw and vibration behaviour. It does not replace a capacity trial on real material, but it exposes most assembly errors before they travel.
| Inspection item | Method / reference | Evidence requested | Acceptance |
|---|---|---|---|
| Structural welds | Visual testing to ISO 17637 with adequate lighting and access | Inspection report and welder qualifications | Compliance with the ISO 5817 quality level named in the contract |
| Coating thickness | Dry film thickness to ISO 2808, ISO 19840 rules on rough surfaces | List of measurement points and gauge calibration record | Specified system and nominal thickness achieved |
| Bought-in components | Nameplate and serial number comparison | Photographed serial numbers of motors, gearboxes and bearings | Identical to the brand and type stated in the offer |
| No-load running | Unloaded run for an agreed duration | Vibration, temperature and current records plus video | No abnormal noise, values inside contractual limits |
| Hydraulics and lubrication | Leak check and pressure reading | Commissioning sheet | No leaks, pressures at design values |
| Spare part lots | Sampling inspection to ISO 2859-1 | Lot size, sample size and acceptance number | Within the chosen acceptance quality limit |
The report: photographs, measurements, signature
An inspection report is not a travel impression. Every item carries the measured value, the name of the person who measured it, the date and a photograph. Non-conformities go into a separate list, each with a correction method, an owner and a date. Whether shipment depends on closing that list must be settled in the contract beforehand, because the moment after inspection is the weakest negotiating position a buyer will ever hold.
Scheduling the supplier factory audit and pre-shipment inspection
Linking inspections to production milestones works better than a single visit before shipment. One check when frame welding is finished, a second at surface preparation before painting, and a final inspection at completed assembly catch faults while they are still cheap. A weld defect found after painting means redoing both the weld and the coating.
Frequently asked questions
What if we cannot travel to the factory?
The inspection can be delegated to an independent body. In that case the checklist, the measurement methods and the acceptance criteria have to be written by the buyer, otherwise the report comes back as a general observation.
Are spare part lots inspected piece by piece?
No. Lots of many identical parts are handled by sampling; the sample size and the acceptance number follow from the lot size.
Should shipment be stopped when a non-conformity appears?
It depends on whether the defect can be corrected on site. Welding and coating issues are repaired at the works, since fixing them in the field is both expensive and usually incomplete.
Audit and inspection are where the acceptance criteria written at bid stage finally take physical form; other articles under procurement and supply deal with the specification and contract side.
Definitions of technical terms: Glossary